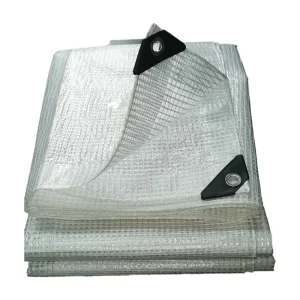
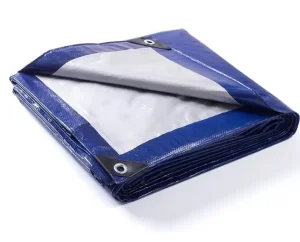
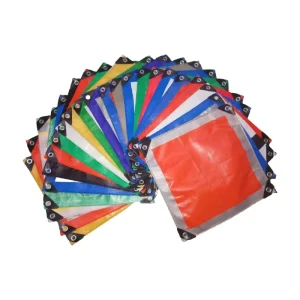
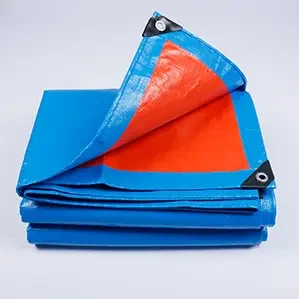
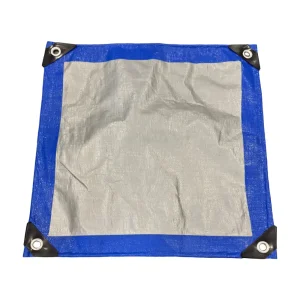
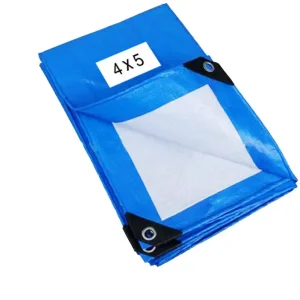
Explore our primary industrial product lines manufactured under rigorous ISO 9001 quality control protocols. High tensile strength, UV-stabilized, and 100% waterproof covers engineered for harsh field environments.
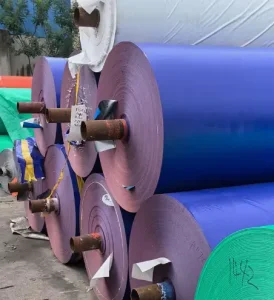
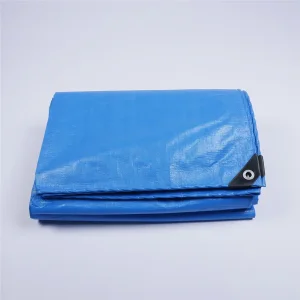
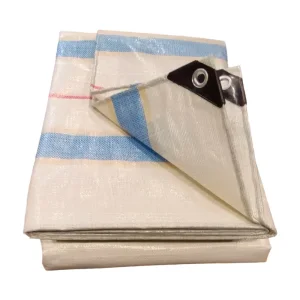
Understanding polymer composition, lamination chemistry, and structural weave mechanics is vital for procurement managers seeking to maximize lifespan while optimizing land and sea freight economics.
Our woven poly tarps feature an ultra-dense High-Density Polyethylene (HDPE) inner scrim woven on high-speed water-jet looms (8x8 to 14x14 mesh density). Double-sided Low-Density Polyethylene (LDPE) molten co-extrusion seals the fabric, providing 100% moisture impermeability and hydrostatic head ratings exceeding 10,000 mm H2O.
Solar radiation rapidly degrades untreated polyolefins via free-radical photo-oxidation. We integrate 3% to 5% high-grade UV Masterbatch (Chimassorb 944 / Tinuvin 770 formulations) directly into the polymer extrudate, guaranteeing weatherability up to 500 KLY (Kilolangleys), extending service life in hot regions such as the Middle East and Australia.
Structural failures start at the edges. Our tarps utilize high-tensile PP perimeter ropes embedded inside ultrasonic heat-sealed hems. Stress points are fortified with heavy-duty molded plastic triangular corner patches and rustproof aluminum or solid brass eyelets punched at precise 50cm or 100cm intervals.
When selecting protective covers for high-stress applications, choosing between PE, PP, and PVC materials determines the total cost of ownership (TCO). The table below outlines structural, thermal, and mechanical parameters for professional procurement evaluation.
| Performance Characteristic | PE Tarpaulin (HDPE/LDPE) | PP Tarpaulin (Polypropylene) | PVC Coated Tarpaulin |
|---|---|---|---|
| Typical Weight Range (GSM) | 60 GSM – 300 GSM | 70 GSM – 260 GSM | 450 GSM – 900+ GSM |
| Tensile Strength (Warp/Weft) | 800 N / 1000 N per 5cm | 950 N / 1150 N per 5cm | 2200 N / 2500 N per 5cm |
| Hydrostatic Pressure Resistance | 8,000 – 12,000 mm H2O | 6,000 – 9,000 mm H2O | > 25,000 mm H2O (100% Impermeable) |
| Flexibility at Low Temperature | Excellent (-40°C to +70°C) | Moderate (-10°C to +80°C) | High (-30°C to +70°C, cold-crack treated) |
| Abrasion & Tear Resistance | Standard to Heavy Duty | High Tensile Stiffness | Extreme / Commercial Vehicle Grade |
| Recyclability & Eco Profile | 100% Recyclable (Code 2 HDPE) | 100% Recyclable (Code 5 PP) | Requires Specialized Recycling |
| Cost / Freight Efficiency | Optimal for High Volume / TCO | Lightweight, Rigid Protection | Premium Investment / Long Service Life |
Centering production in Linyi, Shandong—China's premiere plastics and logistics hub—allows Star Tarpaulins (Linyi Xinshengyang Plastic Products Co., Ltd.) to integrate the entire supply chain from raw resin sourcing to global container shipping.
We source virgin petrochemical resins (Sinopec 5000S HDPE grade) directly to ensure uniform melt flow index (MFI). Modern extrusion drawing lines convert virgin polymer pellets into flat tapes with exact denier control, guaranteeing superior tensile strength before weaving.
Operating over 200 automated circular looms and heavy-duty flat weaving machines, our facility processes millions of square meters per month. Mesh density (e.g., 10x10, 12x12, 14x14 counts) is monitored by optical sensors to eliminate drop-stitches or structural gaps.
Woven substrate rolls pass through high-speed double-sided lamination lines where molten LDPE or PVC is fused under precise temperature and pressure. Inline laser gauge sensors verify uniform coating thickness down to the micron.
By controlling raw granule mixing, yarn drawing, weaving, double-side coating, heat-welding, and automated eyelet punching under one roof, we eliminate third-party sub-contracting markups and quality variance. Batch numbers stamped on every finished roll ensure complete traceability back to the raw material lot.
The industrial tarpaulin market is evolving rapidly toward sustainable polymers, extreme weather protection, and smart tracking integration. Below is our R&D technology development roadmap for global enterprise partners.
To support global carbon reduction targets, our team is pioneering 100% mono-PE recyclable tarpaulins. By aligning the core mesh, lamination film, and edging rope into a single polymer family, worn tarps can be directly re-granulated into post-consumer recycled (PCR) resin without matrix separation.
Integrating nano-TiO2 and fluoropolymer additives into the top LDPE/PVC lamination layer creates self-cleaning, stain-repellent, and anti-fungal surfaces. Dirt, oil, and atmospheric pollutants wash off easily with rainwater, reducing maintenance costs on permanent structures.
For high-value logistics and intermodal container transport, we provide heat-laminated RFID tags and NFC sensors embedded within seam welds. Haulers can track cargo identity, monitor temperature, and record tarp tampering across international transit routes.
Heavy-duty tarpaulins are critical protective assets across global supply chains. Here is how our engineered tarps deliver application-specific advantages.
Temporary weather enclosures keep building projects on schedule. Our flame-retardant (NFPA 701 / DIN 4102 B1 certified) PE and PVC scaffolding covers shield sites from high wind, rain, and debris, while maintaining thermal insulation for concrete curing during winter pours.
Flatbed trailers, cargo containers, and ocean-going deck cargo require tarpaulins that withstand aerodynamic drag and salt spray corrosion. Our double-side coated truck tarps feature heat-welded seams and high tear-propagation resistance under dynamic wind loads.
Protecting harvested grain, hay bales, and silage stacks from moisture infiltration prevents mold and revenue loss. Our UV-stabilized black/silver and green/silver PE covers reflect solar heat to maintain stable internal temperatures while suppressing weeds and algae.
Meeting destination-market regulatory frameworks is critical for seamless customs clearance and commercial risk mitigation. Our products strictly align with major international standards.
Our raw materials comply with EU REACH Regulations (EC) No 1907/2006. All polyolefins, masterbatches, and plasticizers are certified free from Substances of Very High Concern (SVHC), heavy metals (Lead, Cadmium, Mercury), and restricted phthalates.
For North American commercial markets, our fire-retardant tarpaulins pass NFPA 701 (Method 1 & Method 2) and CPAI-84 testing. Products distributed to California comply with California Proposition 65 chemical limits.
Our factory operates under ISO 9001:2015 Quality Management and ISO 14001:2015 Environmental Systems. Every production lot undergoes third-party lab inspection (SGS, BV, TUV) for tensile strength (ASTM D751), tear resistance (ASTM D2261), and hydrostatic head tests.
Volume buyers, hardware retail chains, and government humanitarian agencies require customized packaging, flexible order mixes, and container space optimization to protect margins.
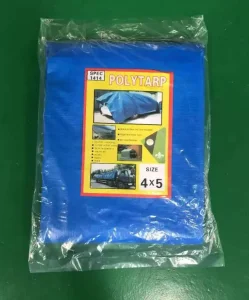
We provide comprehensive OEM packaging solutions. Ready-cut tarps are individual folded, packed in polybags with full-color barcode inserts, display header cards, and master shipping cartons designed for automated distribution centers.
Optimize shipping efficiency by consolidating diverse product lines in a single 20ft or 40ft High-Cube container. Combine PE tarpaulin sheets, tarpaulin rolls, weed barrier fabrics, layflat hoses, and shade meshes to balance inventory turnover.
For bulk commercial buyers and disaster relief tenders, finished tarps are packed into heavy-duty hydraulic press-compressed bales wrapped in woven PE. This increases container loading capacity by up to 35% compared to box packaging.
Direct engineering answers to common procurement, technical specification, and order logistics queries from commercial importers.
Selecting the optimal GSM depends on application longevity, weather exposure, and budget constraints:
We utilize high-grade Hindered Amine Light Stabilizers (HALS) such as Chimassorb 944 and Tinuvin 770 compounded into a carrier resin. For tropical, desert (Middle East/North Africa), or high-altitude regions (Australia/Latin America), we add 3% to 5% UV masterbatch into both the HDPE tape yarn and LDPE film coating. This guarantees UV stability up to 300–500 KLY (Kilolangleys), maintaining over 80% tensile strength after 2 to 5 years of field exposure.
It is crucial to clarify size terminology during contract negotiation:
Standard stock color specifications (e.g., Blue/Silver, Green/Silver, Blue/White) can be ordered in mixed container quantities starting from 3 Metric Tons per specification. Custom colors, brand-printed master cartons, and specialized roll widths require an MOQ of 5 to 10 Tons. Production lead times typically range from 15 to 25 calendar days following artwork confirmation and deposit receipt.
Panels wider than the maximum loom width are joined using continuous automatic high-temperature hot-wedge welding lines. Welding temperature, pressure, and belt speed are digitally controlled to ensure that the molecular bond along the lap seam matches or exceeds the burst tensile strength of the surrounding substrate fabric. Every batch is tested under 10,000 mm H2O hydrostatic head pressure to ensure 100% waterproof integrity.
We routinely support pre-shipment inspections by independent agencies such as SGS, Bureau Veritas (BV), and TÜV Rheinland. We provide ISO 9001 quality compliance certificates, REACH SVHC test statements, RoHS compliance, NFPA 701 fire resistance certificates, and official Bills of Lading accompanied by Form E, Form A, or Certificate of Origin for preferential tariff treatment.
Explore additional specialized tarpaulins, shade meshes, pet shelter covers, and multi-color striped tarpaulin rolls designed for diverse global market requirements.